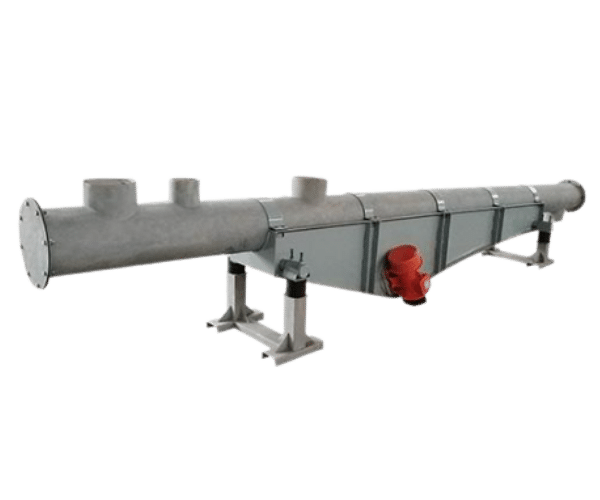
Tubular Feeder
Tubular Vibratory Feeders or Conveyors are designed to convey powders and granules horizontally at a controlled rate in either an open or closed environment. The gentle, low-velocity conveying action operates with no moving parts in contact with the material, ensuring virtually zero product degradation.
Our engineering team works closely with you to custom-design efficient, sanitary vibrating conveyors tailored to your specific application and material handling needs.
Applications & Industries
Vibrating conveyors are highly effective across numerous industries due to the wide variety of material handling processes they can perform.
These conveyors can be mounted on isolation spring support bases or suspended by overhead cables. They are ideal for fragile, agglomerated, or instantized powders, as well as sanitary applications requiring frequent cleaning and low maintenance.
BMPE provides customized vibrating conveyors for a variety of operations, particularly within the following industries:
- Food Processing: Ingredients, milk powder
- Chemicals & Plastics: Polypropylene, chemical powders
Advantages
-
Easily cleaned with no moving parts.
-
With fewer moving parts, vibrating conveyors have easy-to-clean surfaces and require less maintenance than other types of mechanical conveyors.
-
Energy efficient, low-horsepower requirements.
-
Unlike slope models, vibrating conveyors don’t require a ton of horsepower to move materials. Less horsepower leads to energy efficiency and lower operational costs.
-
Extremely quiet operation.
-
An added benefit of the low horsepower requirements is a quiet overall operation, often registering between 60 and 75 A-weighted decibels (dBA).
-
Heavy duty, maintenance-free design.
-
The heavy-duty design allows for continuous operation, protecting against leaks and spillage that can lead to maintenance and downtime.
Get a Quick Quote
Tell us what you need, and our team will get back to you shortly.